




Trampoline Supply Chain: From Raw Materials to Finished Product
Trampoline Supply Chain: From Raw Materials to Finished Product
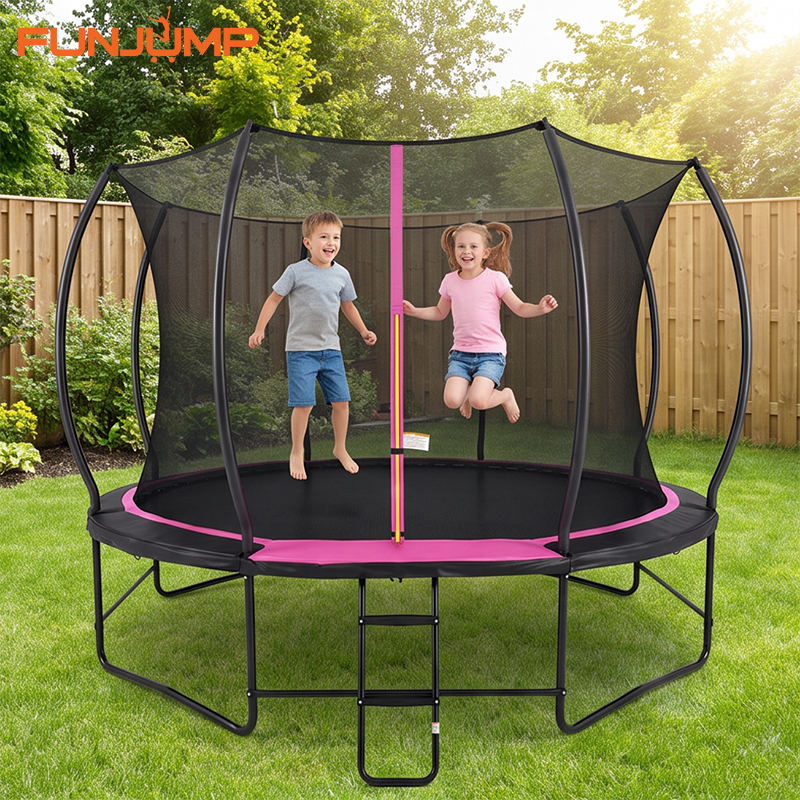
Trampolines have grown into one of the most popular backyard and indoor fitness items for families, gyms and amusement parks across the globe. Most buyers only see the finished, assembled trampoline ready for jumping. Very few stop to consider the long, multi‑step supply chain journey that turns raw steel, woven fabric and foam padding into a safe, durable jumping unit.
Every bounce you enjoy depends on coordinated work across raw‑material suppliers, component workshops, trampoline manufacturers, in‑house testing labs and global logistics teams. Small missteps anywhere in this chain can lead to safety risks, shortened product lifespans or delayed customer shipments. This article walks you through the full trampoline supply chain, starting from incoming raw materials all the way to finished trampolines packed for worldwide delivery, based on real‑world manufacturing practice from Funjump trampoline factory.
Table of Contents
- Understanding Trampoline Supply Chain Basics
- Key Raw Materials That Make Up A Trampoline
- Component Manufacturing: Turning Raw Stock Into Parts
- Factory Assembly & In‑House Production Workflow
- Multi‑Stage Quality Control & Safety Compliance Testing
- OEM / ODM Customization Within The Supply Chain
- Packaging, Logistics & Global Distribution
- Common Supply‑Chain Pain Points For Trampoline Sourcing
- FAQs
- Conclusion
Understanding Trampoline Supply Chain Basics
A complete trampoline supply chain works in sequential phases: raw‑material procurement → component fabrication → factory assembly → safety testing → custom modification (OEM/ODM) → packaging → global shipping. Unlike simple consumer goods, trampolines are hybrid products mixing heavy metal structures, high‑strength textile fabrics, elastic hardware and soft protective foam. Each material category often comes from different specialized upstream suppliers.
Many trampoline factories do not mine or produce every raw material themselves. Instead, they establish long‑term partnerships with certified material vendors, then process, assemble and validate all parts inside their own production facility. This model balances cost efficiency while keeping full oversight over final product safety.
Production timelines shift based on order volume and market seasons. Peak buying seasons (spring and early summer) place heavy pressure on the whole supply network. Material lead‑times, component bottlenecks and lab testing schedules all need careful planning to avoid production slot delays for wholesale buyers.

Key Raw Materials That Make Up A Trampoline
Every trampoline relies on five core groups of raw inputs. Material grade directly defines safety rating, outdoor weather resistance, weight capacity and usable lifespan.
| Component | Core Raw Material | Main Purpose |
|---|---|---|
| Steel Frame & Legs | Q235 galvanized carbon steel pipe | Provides overall structural stability, anti‑rust performance for outdoor backyards |
| Jumping Mat | UV‑stabilized polypropylene (PP) fabric | Absorbs jumping impact, delivers consistent bounce, resists sun fading and tearing |
| Springs / Bungee Cords | High‑carbon spring steel or premium elastic rope | Generates bounce force; spring‑free Mini Trampolines use enclosed bungee cords instead of metal springs |
| Safety Enclosure Net | HDPE high‑density polyethylene woven net | Stops users from falling off the jumping area; mesh design keeps full visibility for parents or supervisors |
| Safety Padding / Foam Sleeves | EPE / EVA foam + PVC cover | Covers springs and metal net poles to prevent hard‑surface injuries during play |
For Outdoor Trampolines, anti‑UV treatment is non‑negotiable for fabric and netting. Without proper UV stabilization, nets and jumping mats will become brittle and tear after several months of direct sunlight exposure. Frame steel must go through galvanization and powder‑coating processes to fight rust from rain and humidity.
Premium factories will request incoming material test reports from each supplier before accepting bulk deliveries. Low‑cost sourcing often cuts corners here: thinner steel wall thickness, lower‑grade fabric without UV treatment or untested foam padding. These material shortcuts create hidden safety hazards for end‑users.
Component Manufacturing: Turning Raw Stock Into Parts
Once raw materials arrive at the trampoline facility, separate production lines turn bulk stock into finished individual components. This intermediate step is critical. Even high‑quality raw steel will fail if bending, welding or sewing is done poorly.
Metal frame processing Steel pipes go through automated cutting, precision bending and punching to create circular or rectangular frame segments, leg supports and net pole tubes. Next comes robotic or semi‑manual welding for connection joints. After welding, frames move to powder‑coating workshops for surface anti‑corrosion finishing. Every weld spot gets visual inspection, and random samples go through load testing to check joint strength.
Spring or bungee component production High‑carbon steel wire is coiled, heat‑treated and galvanized into trampoline springs. Heat treatment is essential: it improves fatigue resistance so springs can handle thousands of repeated jumps without permanent deformation. For spring‑less fitness trampolines, raw elastic cord is cut and enclosed to build silent bungee assemblies.
Textile workshop: jumping mats, safety nets and padding covers Large rolls of PP fabric are computer‑cut to exact mat dimensions. Industrial multi‑needle sewing machines reinforce edges and attach metal D‑rings where springs hook onto the mat. Safety netting is cut and sewn into full enclosure panels with reinforced zipper openings. Foam material is cut to size and wrapped with waterproof PVC fabric to create protective spring covers and pole foam sleeves.
Many trampoline manufacturers source certain pre‑made sub‑components from trusted specialist vendors. Even so, responsible factories still perform incoming QC on all purchased parts before allowing them onto final assembly lines.
Factory Assembly & In‑House Production Workflow
After all separate components pass intermediate checks, they move to final assembly stations. Most consumer‑grade trampolines are not fully pre‑assembled in the factory. Instead, workers complete fit‑checks: verifying every frame piece, mat, spring and net can connect smoothly as designed.
For each unit:
- Frame segments are dry‑fitted together using T‑shape reinforced connectors, checking alignment and connection stability.
- Jumping mat is mounted to test spring hook positions and tension balance across the full mat surface. Uneven spring tension creates unsafe bouncing behavior.
- Safety enclosure poles, net panels, foam sleeves and entry zippers are installed for fit verification.
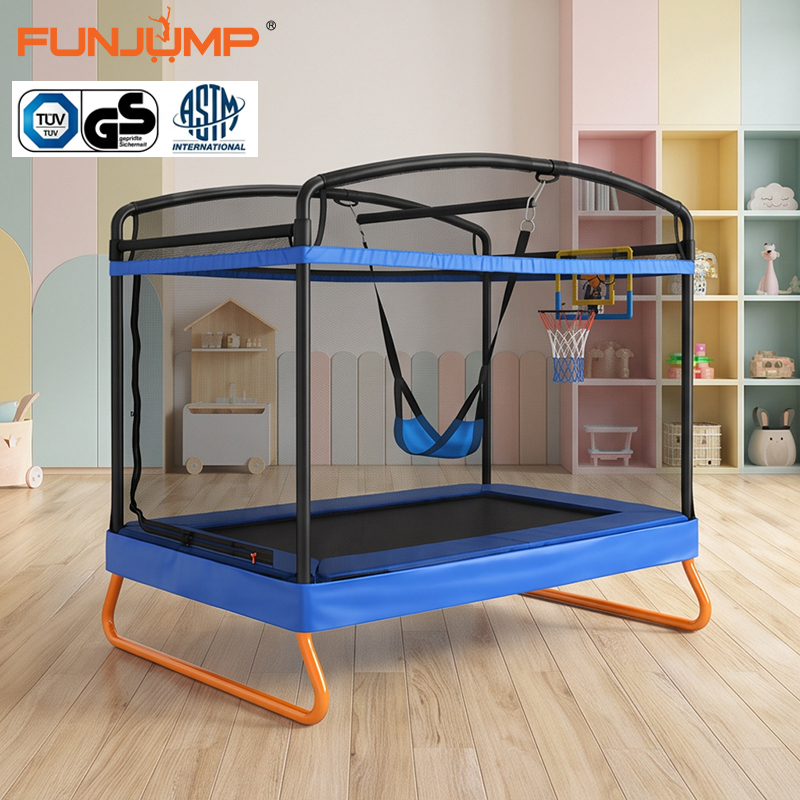
- Accessories such as ladders, basketball hoops, LED light kits or swing attachments are matched to corresponding product models.
Fit‑testing catches dimensional issues early. If parts do not slot together correctly during factory trial assembly, technicians adjust component molds or send defective batches back for rework.
Mini indoor fitness trampolines follow a similar workflow. Hexagonal or octagonal jumping surfaces, adjustable T‑shaped handlebars and rubber non‑slip feet are assembled and checked for wobble and weight‑bearing performance.
Multi‑Stage Quality Control & Safety Compliance Testing
Safety is the highest priority for trampoline manufacturing, as defective units can lead to serious injury risk. Quality control runs across the whole supply chain, not just at final inspection. Funjump maintains its own dedicated trampoline safety‑testing laboratory and specialized inspectors to screen out non‑conforming goods before shipment.
Key inspection stages
- Raw material incoming inspection: Steel thickness, fabric tensile strength, foam density and coating quality are spot‑checked against specification sheets. Material certificates from suppliers are filed for batch traceability.
- First‑article inspection: For every new production batch, the first completed unit undergoes full dimensional and visual review before mass‑production continues.
- In‑process intermediate QC: Weld integrity, sewing seam strength and powder‑coat finish are sampled on each production line shift.
- Lab performance testing: Selected sample units go through static load weight testing, dynamic bounce cycle testing, net tear‑resistance tests and UV aging simulation.
- Pre‑shipment finished‑goods inspection: Random container‑load sampling to verify appearance, part completeness and compliance with design drawings.
To sell into global markets, trampolines must pass third‑party certification audits. Common standards include ISO9001, BSCI, GS, EN71‑14 for Europe, ASTM standards for North America and AS4989 for Australia. These certifications validate that both materials and manufacturing processes meet international safety benchmarks.
Structural gap‑free design is one example of safety‑oriented engineering. Optimized frame‑to‑mat layouts eliminate narrow gaps where children’s fingers or toes could get pinched during play. Double‑zipper plus safety‑buckle door systems prevent accidental openings while jumping. All these features are validated during lab testing before mass production.
OEM / ODM Customization Within The Supply Chain
A major advantage of working with integrated trampoline manufacturers is flexible OEM & ODM services. Custom requests add extra steps into the existing supply chain workflow.
Common customization options include:
- Custom frame, pad or safety‑net color matching
- Printing private‑brand logos on jumping mats, padding or product cartons
- Adjusting product dimensions (sizes ranging from 6ft‑16ft large outdoor trampolines down to 40‑55 inch mini kids trampolines)
- Adding or removing accessories: basketball hoops, sprinkler systems, swing sets, anti‑slip suction feet for indoor children trampolines
- Designing brand‑new model concepts from customer sketches and specifications
The ODM workflow: customer submits requirements → engineering team creates 3D drawings → prototype sample production → lab safety testing of the custom sample → customer sample confirmation → raw‑material re‑sourcing for modified parts → formal mass‑production.
Custom orders extend lead times slightly, since new tooling or special‑run fabrics need to be sourced upstream in the supply chain. Experienced factories will map every change point to ensure custom‑modified products still satisfy all required safety certification rules.
Packaging, Logistics & Global Distribution
After passing all quality checks, trampoline components go into flat‑pack cartons. Trampolines are knock‑down flat‑packed to maximize container loading efficiency. One 20GP shipping container can mix multiple trampoline sizes together. Each carton includes hardware bags, installation manuals and all small accessory pieces.
Finished goods are moved to warehouse storage awaiting container loading. Timely production planning is critical during peak buying periods. If any upstream supply link slows down (for example fabric delivery delays), finished‑goods output drops and may push back vessel booking dates.
From the factory warehouse, containers travel to seaports and ship to buyers in more than 60 countries worldwide. Once imported, wholesalers and retailers unpack the flat‑packed boxes and sell trampolines to end‑users, who complete final home assembly following the provided instruction manual.
Common Supply‑Chain Pain Points For Trampoline Sourcing
Even well‑managed trampoline supply chains face recurring challenges that sourcing buyers should keep in mind.
- Raw‑material price volatility: Steel, textile fabric and foam prices shift with global commodity markets. Long‑term supplier contracts help factories stabilize costs, but sudden price spikes can still impact order budgets.
- Peak‑season capacity pressure: Q1‑Q2 is high‑demand season for trampolines. Material shortages and full‑production‑line schedules can lead to limited available production slots. Many professional buyers place orders months ahead to secure manufacturing capacity.
- Sub‑component bottlenecks: Certain specialized parts such as certified high‑tension springs or UV‑treated safety netting can become supply‑constrained.
- Compliance documentation risks: Some low‑grade suppliers provide counterfeit certification documents. Reputable manufacturers support third‑party audit visits and can provide full, verifiable test‑report files for every product series.
- Logistics disruptions: Port congestion, ocean‑freight cost swings and customs clearance delays can add extra lead‑time beyond factory production days.
Working with a vertically integrated trampoline factory with in‑house testing capabilities helps mitigate most of these risks compared to sourcing from middleman trading companies without direct production oversight.
FAQs
What is the most critical raw material for trampoline safety?
Every component matters. However, frame steel grade and wall thickness, plus UV‑resistant jumping mat fabric are two top items. Weak steel frames create major collapse hazards, while poor‑quality fabric will tear quickly under repeated jumping.
How does OEM customization affect trampoline supply‑chain lead time?
Simple customizations like logo printing add roughly 7‑14 working days. Full ODM new‑model development with prototyping can take 30‑60 days before mass‑production can start. Complex custom projects need early communication between buyer and engineering team.
Why is in‑house safety lab testing important for trampoline manufacturers?
Third‑party certification happens periodically. Day‑to‑day batch‑level quality screening needs to happen inside the factory. An on‑site lab allows manufacturers to catch material drift or process problems on‑going without waiting for external lab turnaround times.
What causes trampoline supply delays in peak seasons?
Delays typically stem from upstream raw‑material delivery bottlenecks, fully occupied production lines, or shortage of certified testing capacity. Advanced order planning is strongly recommended for wholesale trampoline buyers.
Are all trampoline components manufactured inside one factory?
Not always. Many factories purchase certain specialized sub‑parts, but responsible manufacturers will perform strict incoming QC for every bought‑in component. Complete traceability documentation for all materials should be available upon buyer request.
Conclusion
The trampoline supply‑chain journey from raw steel rolls and textile fabric to a finished jumping product is far more complex than most customers realize. It combines metal engineering, textile manufacturing, foam processing, multi‑layer safety testing and global logistics management.
Every safe, fun trampoline you see on the market is the output of tightly coordinated upstream suppliers, disciplined factory workflows and rigorous quality checks at each production stage. Understanding this end‑to‑end process helps wholesale buyers make smarter sourcing decisions, evaluate real factory capabilities and recognize where cost‑cutting shortcuts can compromise product safety.
Whether you are sourcing standard‑model trampolines or developing custom OEM trampoline lines, prioritizing supply‑chain transparency, mate